
Flame Proof Hoists Manufacturer in India
Industrial places that work with gases, vapours or dust need lifting equipment that is made to deal with the dangers in their area. Modheshwari Engineering & Fabricators. Provides Flame Proof Hoists for industries where lifting tools that prevent explosions might be needed. These hoists are chosen based on the type of area how much weight they can lift how high they can lift and the conditions where they will be used.
As a Flame Proof Hoists Manufacturer we pay attention to the setups for the equipment safe lifting of heavy things and electrical parts that protect in the dangerous area. Choosing the hoist depends on what it will be used for which area it is in how often it will be used and the safety rules that apply.
Our answers also help companies that need a Flame Proof Hoists Supplier for lifting tasks, in industrial areas.
What are Flame Proof Hoists?
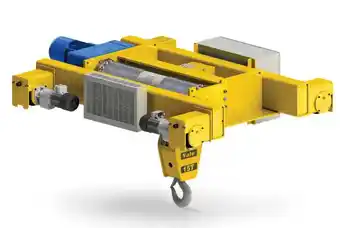
Flame Proof Hoists are lifting devices made to work in places that have gases, vapours or combustible dust. Flame Proof Hoists are designed to be safe when fire or explosions could happen.These places can easily catch fire so the hoists are specially made to be safe. Based on their design and certification Flame Proof Hoists have enclosures and electrical parts that are meant to prevent any spark from igniting the air around them. This helps keep the area safe, from fire or explosion.
Flame Proof Hoists may have a protected motor, braking system, lifting mechanism, hook assembly and suitable control equipment. Depending on the job Flame Proof Hoists can be set up with a wire rope or chain lifting setup. Joined to a matching crane system.
The right equipment must be chosen based on the hazardous area classification, the gas group or dust group the temperature needs and the applicable standards.A regular industrial hoist should not be taken as suitable, for an area unless it has the necessary assessment and certification.
Specialized Hazardous-Area Lifting
Flame Proof Hoists for Industrial Applications
Facilities handling combustible materials need lifting equipment that matches the conditions of their operating environment. Flame-proof hoists are used where the area classification and risk assessment call for appropriately protected lifting equipment.
Our Flame Proof Hoists can be considered for applications such as:
Petrochemical processing facilities
Oil and gas installations
Paint and coating plants
Chemical manufacturing units
Solvent storage and handling areas
Gas processing installations
Flammable material warehouses
Pharmaceutical production facilities
Process equipment maintenance
The appropriate hoist configuration depends on the area classification, lifting capacity, lifting height, operating frequency, temperature class and required protection certification. These details should be confirmed before selecting equipment for a hazardous location.
Flame Proof Hoists Supplier & Exporter in India
As a Flame Proof Hoists Supplier, Modheshwari Engineering & Fabricators caters to industrial projects that require lifting equipment for designated hazardous areas. Hoist selection can be based on the material being handled, site classification, load requirements, operating conditions and the crane or support arrangement.
Our Flame Proof Hoists India solutions can be considered for industrial facilities where suitable explosion-protected lifting equipment is specified. Customers can share their technical requirements to help determine the appropriate configuration and applicable protection standards.
As a Flame Proof Hoists Exporter, we also cater to international project enquiries. Export requirements can be looked at based on the rules of the country where the product is going. It is important to check if the area is a place. Also make sure all the needed papers are, in order.Think about how much weight the equipment can lift. Check the power it needs to work. Look at the details of the project. Make sure the equipment is right, for the job. Make sure it has the papers before putting it in place.
Key Features of Crane Hoists
01
Protective enclosure options for specified hazardous environments
02
Lifting capacity selected for the application
03
Suitable wire rope or chain hoist configurations
04
Protected electrical components, as specified
05
Braking arrangements suited to the hoist design
06
Options for different lifting heights
07
Integration options for suitable crane systems
08
Compatible control arrangements for hazardous locations
09
Configuration based on applicable protection standards
10
Designed for specified industrial operating conditions
